Open
a
better
future
Electrolytes

- TECHNOLOGY
- Electrolytes
Empowering Industries with Advanced Solutions
01
Electrolytes
Chemical batteries can be categorized into 2 different types of battery: ① a primary battery that converts chemical energy into electric energy for a singular use and ② a secondary battery that can be continuously used by repeating charging and discharging. Secondary batteries can be used in small devices such as mobile phones and laptops to larger scale devices such as ESS and electric vehicles, and it can also be utilized in innovative devices such as wearable devices and mobile healthcare. The four main components that make up these secondary batteries are: Cathode, Anode, Separators, and Electrolytes; electrolytes facilitate the movement of lithium ions between the cathode and the anode, and serves an important role in maintaining stability in batteries.
Electrolytes consist of three components in lithium salts, solvents, and additives. Lithium salts provide electric and chemical stability in electrolytes. Solvents are responsible in dissolving these lithium salts, and determine the ion conductivity, viscosity, and density of the electrolyte. Additives provide support in various areas such as safety, performance at extreme temperatures, and general performance. DS Electera is continuously developing ways to improve its high performance and high quality electrolytes, and is leading electrolyte business through innovations.
-
02Electrolyte's Functions
Electrolyte's function in a lithium ion battery
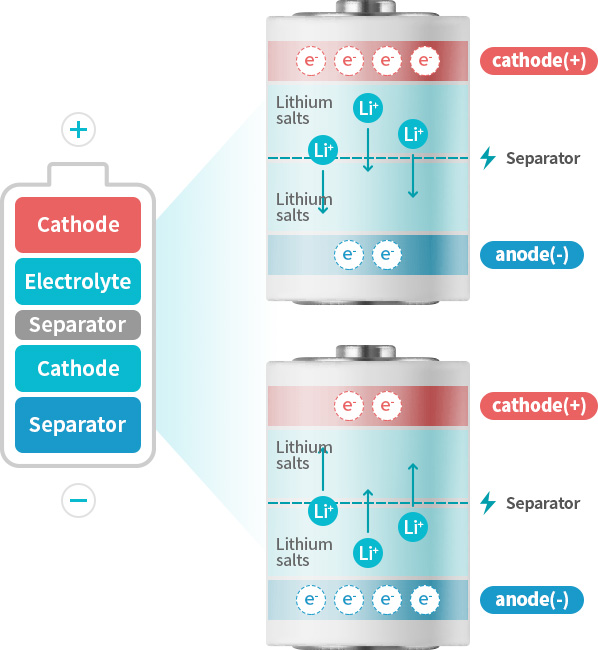
- Charge
- The lithium ion (Li+) in the cathode(+) moves to the anode(-)
- Discharge
- The lithium ion (Li+) in the anode(-) moves to the cathode(+)
-
03Electrolyte Production
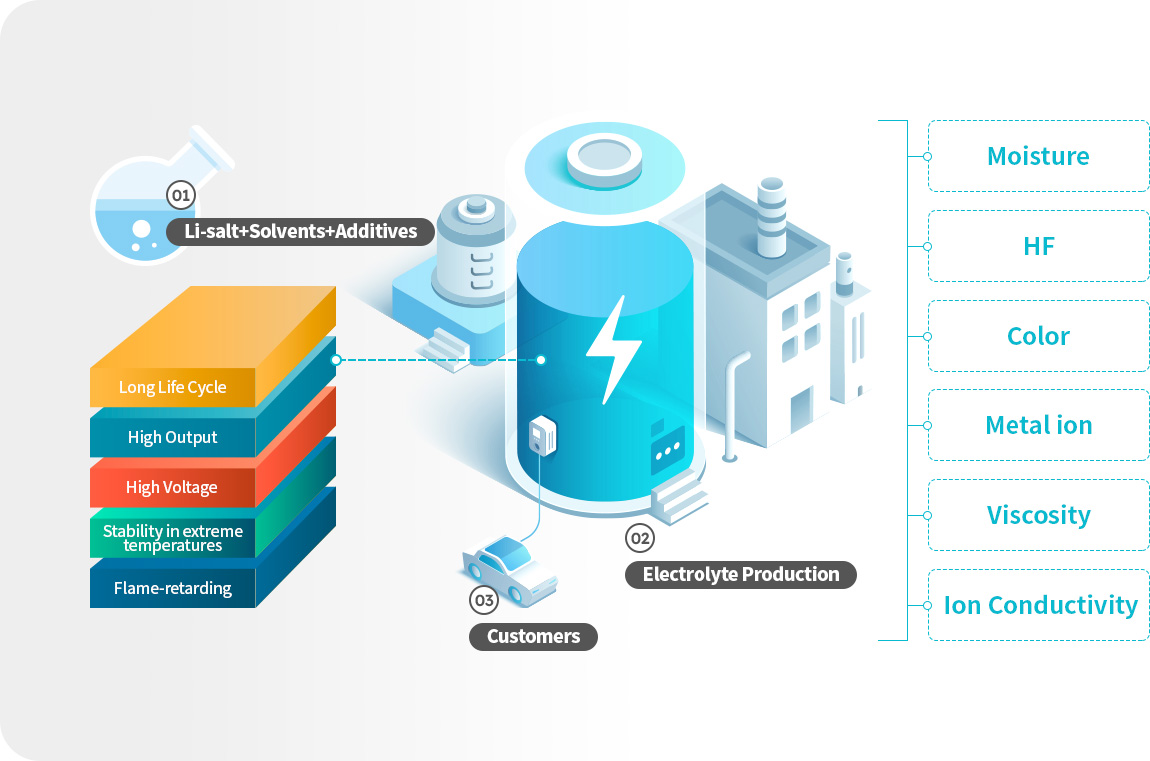
04
Enhanced Electrolyte Production Process
Established an In-Line System to inhibit exposure to the atmosphere from material unloading to product shipping, and the process is centrally controlled through HMI System to ensure consistant high quality products at competitive pricing.
-
Moisture RemovalMixing
-
Raw material stockingCharging/Packing
-
Raw material inputShipping/Canister Cleaning

- Can supply in both ISO
Tanks and Canisters - Packaging according to
customers' needs
Moisture Removal
Enhanced quality management through adopting moisture removal system with
sight glass; Established precise process control through HMI System
sight glass; Established precise process control through HMI System
-
 - Sight glass
-
 - HMI System central control
-
 - Precise temperature control
Mixing
Room for human error is minimized for Mixing and Production by automation, and quality is improved through intensified material receiving
inspection compared to our competitors. Samples are taken automatically for each production step to prevent any quality mishaps.
inspection compared to our competitors. Samples are taken automatically for each production step to prevent any quality mishaps.
-
 - In-Line sampling system
-
 - Automated temperature control
Raw material
stocking
stocking
Secured storage tank and warehouse for large amount of raw material stocking; established In-Line System to minimize exposure
to the atmosphere. Also able to store liquefied Li-Salt.
to the atmosphere. Also able to store liquefied Li-Salt.
-
 - Prolonged storage capability
-
 - In-Line System
-
 - Liquefied Li-Salt
Charging/Packing
Automated charging & packaging system prevents contamination and ensures
best electrolyte product quality.
best electrolyte product quality.
-
 - Automated charging
-

-
 - Automated packaging
Raw material input
Subdivision of powder material takes place in a Purge Box located in the Dry Room to minimize contamination, and liquid materials are input in
an In-Line System to mitigate any contamination risks. HMI System makes sure there are no input errors when raw materials are added.
an In-Line System to mitigate any contamination risks. HMI System makes sure there are no input errors when raw materials are added.
-
 - Optimal production environment
-
 - Automated material input (errors prevented)
-
 - Input errors controlled <2kg
Shipping/Canister
Cleaning
Cleaning
With the most intense filter system and number of inspection points in the industry, we've enhanced our quality level; with the introduction
of automated canister cleaning equipment, we've preemptively prevented any errors that may be related to the canisters.
of automated canister cleaning equipment, we've preemptively prevented any errors that may be related to the canisters.
-
 - Strengthened inspection
-
 - Large scale low-temperature warehouse
-
 - Automated canister cleaning


HQ / R&D Center 165, Namgongjusandan-gil, Gongju-si, Chungcheongnam-do, Republic of Korea
USA Plant 298 Frank Martin Rd, Shelbyville, TN 37160, United States
Tel +82 41-840-7300 FAX +82 41-852-7425
USA Plant 298 Frank Martin Rd, Shelbyville, TN 37160, United States
Tel +82 41-840-7300 FAX +82 41-852-7425
Copyright ⓒ 2024 Duksan Electera Co., Ltd. ALL RIGHTS RESERVED.